
The Role of Luxury Stone Crusher Plant Manufacturers in Modern Industrial Aggregates Production
Introduction
In the global construction, mining, and infrastructure sectors, the demand for high-quality aggregates is relentless. From the concrete foundations of skyscrapers to the asphalt of transcontinental highways, crushed stone serves as the literal bedrock of modern civilization. Within this industrial ecosystem, a specialized segment has emerged: the luxury stone crusher plant manufacturer. Unlike mass-market suppliers that prioritize volume over precision, these manufacturers cater to clients who demand exceptional throughput, superior end-product shape, minimal downtime, and long-term operational cost efficiency. This article provides a detailed, objective analysis of what defines a luxury stone crusher plant manufacturer, the engineering principles that distinguish them, and their strategic importance in high-stakes quarrying and mining operations.
Defining the Luxury Segment in Crushing Equipment
The term “luxury” in heavy industrial machinery does not imply ornamental excess. Rather, it denotes a convergence of high-performance engineering, premium materials, advanced automation, and bespoke service. A luxury stone crusher plant manufacturer typically operates at the apex of the market, offering plants that are:
These manufacturers do not compete on price per ton of machine weight. Instead, they compete on total cost of ownership, reliability, and the ability to deliver a consistent, cubical aggregate product that commands higher market prices.
Key Engineering Differentiators
To understand what makes a luxury plant luxurious, one must examine its core subsystems.
1. Crushing Chambers and Wear Materials
A luxury manufacturer invests heavily in metallurgy. Jaw crushers may use manganese steel with optimized alloying elements (e.g., Mn18Cr2 with titanium additions) to extend wear life by 30–50% compared to standard plates. Cone crushers—often the heart of secondary and tertiary stages—feature bronze bushings, hydraulic tramp release, and automated setting adjustment (ASRi). For impact crushers, ceramic blow bars and high-chrome alloys are standard. The result is not merely longer life but consistent gradation, which reduces recirculating loads and energy consumption per ton.
2. Screening and Classification Precision
Luxury plants integrate high-efficiency banana screens or elliptical motion screens with polyurethane or rubber media. These units achieve separation efficiencies above 95%, minimizing misplaced material. Some manufacturers incorporate air classifiers or water-based washing systems to remove microfines, producing washed aggregates for premium concrete applications.
3. Automation and Digital Twin Technology
A defining feature of luxury manufacturers is the integration of SCADA (Supervisory Control and Data Acquisition) systems. Operators can monitor bearing temperatures, oil pressure, vibration signatures, and throughput from a central control room or a mobile device. Advanced plants use digital twin models to simulate wear and predict component failure, allowing planned maintenance windows rather than reactive breakdowns. This level of automation reduces human error and increases plant availability to over 95%.
4. Structural Integrity and Modular Design
Luxury plants are often modular, allowing rapid relocation without cutting and re-welding main frames. Chassis are stress-relieved and shot-blasted before painting with marine-grade epoxy. Bolt-on rather than weld-on components facilitate field replacement. This design philosophy reduces installation time by 40–60% and ensures structural longevity even in corrosive or high-altitude environments.
The Manufacturer’s Role: Beyond Fabrication
A true luxury manufacturer acts as a solutions partner, not merely a vendor. The process typically follows these stages:
This holistic approach explains why a luxury plant may cost 30–100% more upfront but delivers a payback period of 18–36 months through higher availability and lower energy per ton.
Economic and Operational Justification
Critics may argue that luxury plants are overkill for small quarries. However, for large-scale operations—such as those supplying ballast for high-speed rail, aggregates for ready-mix concrete in megacities, or manufactured sand for hydropower dams—the economics are compelling. Consider a 500 tph granite plant:
Additionally, luxury plants produce better-shaped aggregates (cubicity > 85%), which reduce cement content in concrete by 5–8%, lowering the carbon footprint of construction.
Environmental and Sustainability Considerations
Modern luxury manufacturers are also leaders in sustainability. They incorporate:
These features are not merely regulatory compliance; they are increasingly required by ESG-focused investors and large construction clients.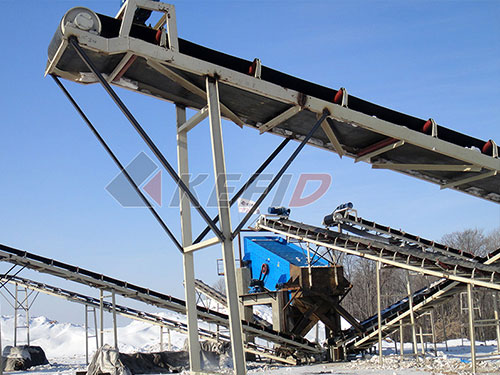
Global Landscape of Luxury Manufacturers
While many companies fabricate crushers, only a handful qualify as luxury stone crusher plant manufacturers. These include established European brands (e.g., Metso Outotec, Sandvik, thyssenkrupp) and select Asian manufacturers that have adopted European quality standards (e.g., SBM, Liming Heavy Industry, Shanghai Zenith). The common thread is vertical integration: they control casting foundries, machining centers, and R&D labs. They also maintain global service networks with guaranteed response times (e.g., 24 hours in North America, 48 hours in Africa).
Challenges and Limitations
Luxury plants are not without drawbacks. Lead times can extend to 6–12 months due to custom engineering. Spare parts may be proprietary and expensive. The complexity of automation requires skilled operators, which may be scarce in remote regions. Finally, the high capital cost can be a barrier for small-to-medium enterprises. Therefore, a luxury manufacturer must clearly communicate value proposition and offer flexible financing or rental options.
Conclusion
The luxury stone crusher plant manufacturer occupies a vital niche in the aggregates industry. By prioritizing engineering excellence, digital integration, and lifetime support, these manufacturers enable quarry operators to achieve higher productivity, superior product quality, and lower long-term costs. While the initial investment is substantial, the return on investment—measured in availability, energy efficiency, and market premium—justifies the expenditure for large-scale, high-stakes operations. As global infrastructure demands grow and environmental regulations tighten, the luxury segment will likely set the benchmark for all crushing equipment. For any serious aggregate producer, partnering with a luxury manufacturer is not an extravagance; it is a strategic decision that pays dividends for decades.
If you have any questions about our products, please feel free to contact us. We take all inquiries and suggestions very seriously.