
Here is a detailed, professional, and objective article on the Slag Crusher Plant Fabricator Specification.
The efficient processing of industrial slag—a byproduct of metallurgical operations, incineration, and power generation—is a critical component of modern waste management and resource recovery. A slag crusher plant is not a singular machine but an integrated system designed to reduce large, abrasive, and often heterogeneous slag lumps into uniform, saleable, or disposable aggregates. The specification of the fabricator responsible for constructing this plant is as crucial as the specification of the plant itself. This article provides a detailed, objective framework for the technical and commercial specifications that define a qualified slag crusher plant fabricator. It covers the scope of supply, material selection, fabrication standards, quality assurance protocols, and performance guarantees essential for procurement engineers, project managers, and metallurgical plant operators.
Slag, whether derived from steelmaking (BOF, EAF), blast furnaces, or municipal solid waste incineration, presents unique challenges. It is typically hard, abrasive, and may contain metallic inclusions, requiring robust crushing and separation equipment. A slag crusher plant fabricator must therefore possess not only general fabrication capabilities but also specialized knowledge in wear-resistant materials, dust suppression, and magnetic separation integration.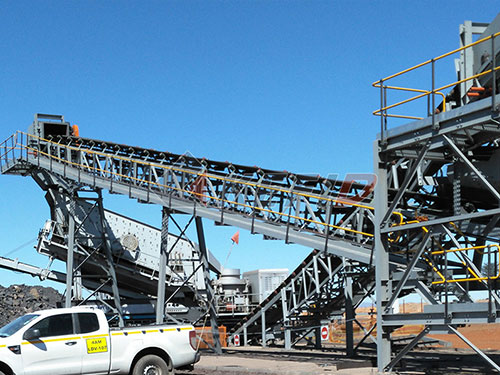
The specification of a fabricator is the contractual bridge between the plant owner’s process requirements and the physical reality of the constructed facility. An incomplete or ambiguous fabricator specification invariably leads to project delays, cost overruns, and premature equipment failure. This article delineates the mandatory and optional elements of such a specification.
The fabricator’s scope must be explicitly defined. A typical specification divides the scope into the following categories:
The fabricator shall be responsible for the detailed design of the plant, including:
The fabricator shall manufacture or procure the following core components:
The fabricator’s responsibility extends to site erection, alignment, grouting, and trial runs. The specification must state whether the fabricator provides supervisory services only or a full turnkey erection team.
Slag is highly abrasive. Therefore, the fabricator’s material selection is the single most important technical specification.
The fabricator must adhere to:
A fabricator specification must include measurable performance guarantees. These are typically backed by a performance bond.
The plant shall process a minimum of [X] tonnes per hour of slag with a bulk density of 1.6 t/m³ and a moisture content of up to 5%. The fabricator must guarantee this capacity over a continuous 8-hour shift.
The final product shall have a particle size distribution such that 95% passes a 40 mm screen and 100% passes a 75 mm screen. The fabricator must provide a sieve analysis curve from a certified test run.
The magnetic separator shall recover at least 98% of ferrous metal content greater than 10 mm. The recovered metal shall have a purity of at least 90% iron.
Before shipment, the fabricator shall conduct a FAT on all rotating equipment. The FAT protocol must include:
The fabricator must operate under a documented Quality Management System, preferably certified to ISO 9001:2015.
All pressure parts and wear liners shall be traceable to mill test certificates (EN 10204 3.1). The fabricator shall maintain a traceability matrix linking each component to its heat number.
The fabricator shall deliver three hard copies and one digital copy of: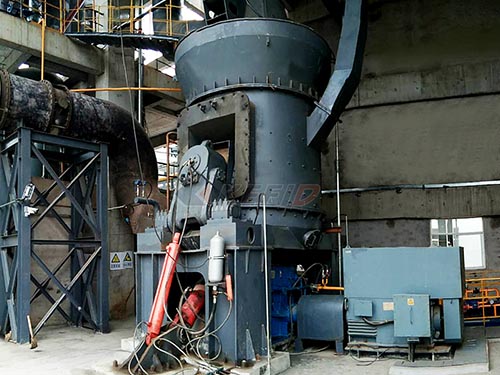
The specification must mandate a recommended spare parts list for two years of operation. This includes:
The fabricator shall guarantee availability of spare parts for a minimum of ten years. Response time for a field service engineer shall not exceed 48 hours from notification.
The fabricator specification must include:
The specification of a slag crusher plant fabricator is a multi-disciplinary document that bridges metallurgy, mechanical engineering, structural design, and contract law. A rigorous specification—covering material hardness, fabrication tolerances, performance guarantees, and documentation—is the only reliable method to ensure that the delivered plant can withstand the extreme abrasiveness of slag while meeting throughput and recovery targets. Procurement teams must treat the fabricator specification not as a formality but as the primary risk mitigation tool. By adhering to the framework outlined above, project stakeholders can achieve a slag processing facility that operates safely, efficiently, and profitably for decades.
If you have any questions about our products, please feel free to contact us. We take all inquiries and suggestions very seriously.