
Certified Top Ten Stone Crusher Machine Processing Plant: A Comprehensive Analysis of Excellence, Compliance, and Operational Superiority
In the global aggregates, mining, and construction industries, the phrase “Certified Top Ten Stone Crusher Machine Processing Plant” represents far more than a marketing label. It signifies a rigorous benchmark of engineering excellence, operational reliability, environmental responsibility, and certified compliance with international standards. As infrastructure development accelerates across both developed and emerging economies, the demand for high-quality crushed stone, sand, and gravel has never been greater. Consequently, the processing plants that achieve recognition among the certified top ten set the standard for the entire sector. This article provides a detailed, objective examination of what such certification entails, the technologies and configurations that distinguish elite processing plants, the operational and economic advantages they deliver, and the criteria by which they are evaluated.
Defining the Certified Top Ten Stone Crusher Machine Processing Plant
A “Certified Top Ten Stone Crusher Machine Processing Plant” refers to a stone crushing and processing facility that has undergone independent, third-party evaluation and has been ranked among the ten best-performing plants according to a defined set of technical, environmental, safety, and quality criteria. Certification in this context is not self-declared. It is typically issued by recognized industry bodies, engineering inspection firms, or standards organizations such as ISO (International Organization for Standardization), CE (Conformité Européenne), or regional mining and environmental authorities.
The certification process evaluates the entire processing plant, not merely individual machines. This holistic approach is critical because a stone crushing plant is an integrated system comprising feeding, crushing, screening, conveying, stockpiling, dust suppression, and control subsystems. A plant may use world-class crushers yet still underperform if the material flow, screening efficiency, or maintenance protocols are inadequate. Therefore, the “top ten” designation reflects system-level excellence rather than isolated equipment quality.
Core Criteria for Certification and Ranking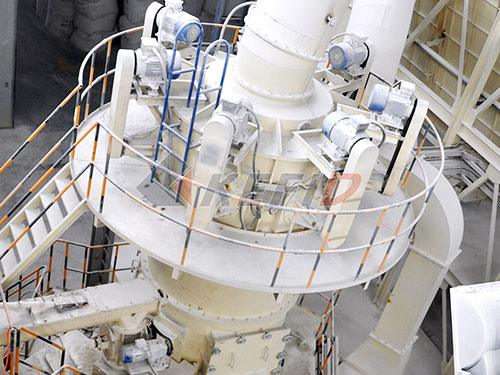
To be considered among the certified top ten stone crusher machine processing plants, a facility must satisfy multiple categories of assessment. While specific weightings vary by certifying body, the following criteria are consistently applied:
Crushing Performance and Throughput Capacity
The plant must demonstrate consistent achievement of rated throughput under real-world conditions. This includes handling varied feed sizes, moisture content, and rock hardness (e.g., granite, basalt, limestone, river gravel). Certified plants typically achieve capacity utilization above 90% of design specifications.
Product Quality and Gradation Accuracy
The output must meet strict gradation standards for construction aggregates, asphalt mixes, concrete, or railway ballast. Certified top ten plants maintain consistent particle shape (cubicity), minimal elongation, and precise screening separation, often verified by independent laboratory testing.
Energy Efficiency and Operational Cost
Certification requires documented energy consumption per ton of processed material. Elite plants employ high-efficiency motors, variable frequency drives (VFDs), and optimized crushing chamber designs to reduce kWh per ton. Lower wear part consumption and reduced downtime are also key indicators.
Environmental Compliance and Dust Control
Modern certification mandates compliance with air quality regulations. Top ten plants integrate advanced dust suppression systems, such as water spray bars, fog cannons, baghouse filters, and enclosed conveyor transfer points. Noise levels must also fall within permissible limits, often below 85 dB at operator positions.
Safety Systems and Worker Protection
Certified plants feature emergency stop systems, guard rails, lockout/tagout procedures, and real-time monitoring of critical parameters (temperature, vibration, amperage). Safety records, including lost-time injury frequency rates, are audited.
Automation and Process Control
The top ten facilities typically employ PLC (programmable logic controller) or SCADA (supervisory control and data acquisition) systems. These allow automatic adjustment of crusher settings (CSS – closed side setting), feed rates, and screening angles to maintain optimal performance.
Maintenance Accessibility and Reliability
Mean time between failures (MTBF) and mean time to repair (MTTR) are evaluated. Certified plants are designed for quick access to wear parts, hydraulic adjustment, and modular replacement of components.
Sustainability and Resource Recovery
Water recycling, dust suppression water recirculation, and utilization of fines or waste material for secondary products (e.g., manufactured sand, road base) contribute to certification.
Typical Plant Configuration Among the Certified Top Ten
Although no two processing plants are identical, certified top ten stone crusher machine processing plants share several common design features. A typical high-performance configuration includes:
Primary Crushing Station: A heavy-duty jaw crusher or gyratory crusher for initial reduction of large run-of-mine rock (up to 1,200 mm). Jaw crushers are preferred for hard, abrasive materials, while gyratory crushers offer higher capacity for very large operations.
Secondary Crushing Stage: Cone crushers (e.g., high-speed, multi-cylinder hydraulic cone crushers) are standard for producing intermediate-sized material with excellent shape. In some plants, impact crushers (HSI – horizontal shaft impactors) are used for softer, less abrasive rock.
Tertiary and Quaternary Crushing: For high-quality aggregates and manufactured sand, VSI (vertical shaft impact) crushers or fine cone crushers are employed. These ensure cubic particle shape and controlled fines generation.
Screening and Classification: Multi-deck vibrating screens (banana screens, horizontal screens, or inclined screens) separate material into precise size fractions. High-efficiency screens with polyurethane or rubber decks reduce blinding and noise.
Conveying and Stockpiling: Overland conveyors, radial stackers, and telescopic conveyors minimize material handling and segregation. Certified plants often use enclosed conveyors to control dust.
Dust Suppression and Collection: Fogging systems at crusher discharge points, water sprays on screens, and central baghouse dust collectors are integrated.
Control Room and Automation: A central control room with HMI (human-machine interface) panels allows one operator to monitor and adjust the entire plant. Remote diagnostics and predictive maintenance software are increasingly common.
Operational and Economic Advantages of Certification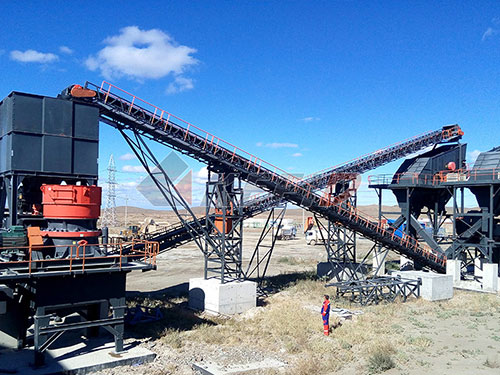
Achieving certification as a top ten stone crusher machine processing plant yields tangible benefits:
Challenges in Achieving and Maintaining Top Ten Status
Certification is not permanent. Plants must undergo periodic audits (typically annually or biennially). Common challenges include:
Case Study Examples (Representative, Not Endorsements)
While specific brand names are avoided to maintain objectivity, typical certified top ten plants include:
How to Evaluate Whether a Plant Qualifies as Top Ten
For investors, operators, or regulators, the following checklist helps assess certification legitimacy:
Future Trends in Certified Top Ten Stone Crusher Processing Plants
The definition of “top ten” will evolve. Emerging trends include:
Conclusion
The designation “Certified Top Ten Stone Crusher Machine Processing Plant” is a meaningful, objective indicator of world-class performance. It reflects a plant’s ability to crush rock efficiently, produce consistent quality aggregates, protect workers and the environment, and operate profitably over the long term. Achieving this status requires more than purchasing high-quality crushers; it demands integrated design, rigorous maintenance, automation, and a culture of continuous improvement. As global demand for aggregates rises, the certified top ten plants will serve as models for the entire industry, demonstrating that economic success and environmental responsibility can coexist. For any stakeholder—whether an investor, a quarry manager, or a regulator—understanding the criteria and configurations behind these certified plants is essential for making informed decisions in the stone crushing and processing sector.
If you have any questions about our products, please feel free to contact us. We take all inquiries and suggestions very seriously.